Pawsome-Specializing in vet health products since 2015
China’s drill head manufacturing sector serves mining, construction, geothermal, water-well, and directional drilling projects worldwide. Choosing a supplier requires more than comparing factory prices. The correct Drill Head must match rock hardness, formation abrasiveness, torque, flushing method, and rig compatibility. A polished catalogue cannot reveal everything.
Industry demand supports careful sourcing. The International Energy Agency’s Global Critical Minerals Outlook 2024 reported that lithium demand grew by about 30% in 2023. Demand for nickel, cobalt, graphite, and rare earth elements also increased. These trends encourage deeper exploration and more demanding drilling conditions. The U.S. Geological Survey’s Mineral Commodity Summaries 2025 further shows China’s major role in several mineral supply chains. More exploration creates opportunities for Chinese manufacturers, but it does not make every supplier equally reliable.
Look for evidence, not slogans. Review material certificates, heat-treatment records, thread tolerances, and documented field performance. Ask whether the manufacturer tests button retention, impact resistance, and water-flow stability. A carbide insert may look perfect under bright factory lighting, yet fail after several hours in fractured granite. Independent inspection can reduce that risk. ISO 9001 certification is useful, but it does not replace application-specific testing. Export experience, spare-part availability, response time, and warranty terms also matter. No universal ranking exists. “Top” depends on your formation, rig, budget, and operating region. This guide examines how to compare China’s leading Drill Head manufacturers with practical, verifiable criteria. Some assumptions may need revision after field trials. That is normal. Performance data should decide.
A drill head is the working assembly that holds or guides a cutting tool during drilling. It transfers rotation, pressure, and cooling control into the material. In practical terms, it may include a chuck, spindle, bearing system, and replaceable cutting interface. The exact structure depends on the machine and drilling task.
Drill heads are used in construction, mining, road maintenance, water-well work, and factory machining. A compact head can bore clean holes in steel plates. A heavy-duty head may cut through concrete, rock, or layered ground.
Different materials require different torque, speed, cooling, and bit compatibility. Choosing only by appearance is risky. I have seen operators select a powerful head that overheated because its cooling path was poorly matched to the job.
Check the required hole diameter, depth, material hardness, and machine connection before comparing suppliers. Verify spindle accuracy, bearing protection, replacement-part access, and operating temperature limits. Ask for measurable data, such as runout tolerance and recommended rotation speed. These details reveal more than a polished product description.
Field conditions also matter. Dust, vibration, water, and limited maintenance can shorten service life quickly. A head designed for a clean workshop may perform poorly underground. The most expensive option is not always the best choice. Sometimes, a simpler head with accessible parts delivers more reliable work. Misjudging that trade-off can become an expensive lesson.
Chinese manufacturers produce several drill head types for metal, concrete, wood, and geological work. Twist drill heads suit general metal drilling and offer simple chip removal. Step drill heads create several hole sizes with one tool. They work well on thin sheet metal, though excessive pressure can damage the steps.
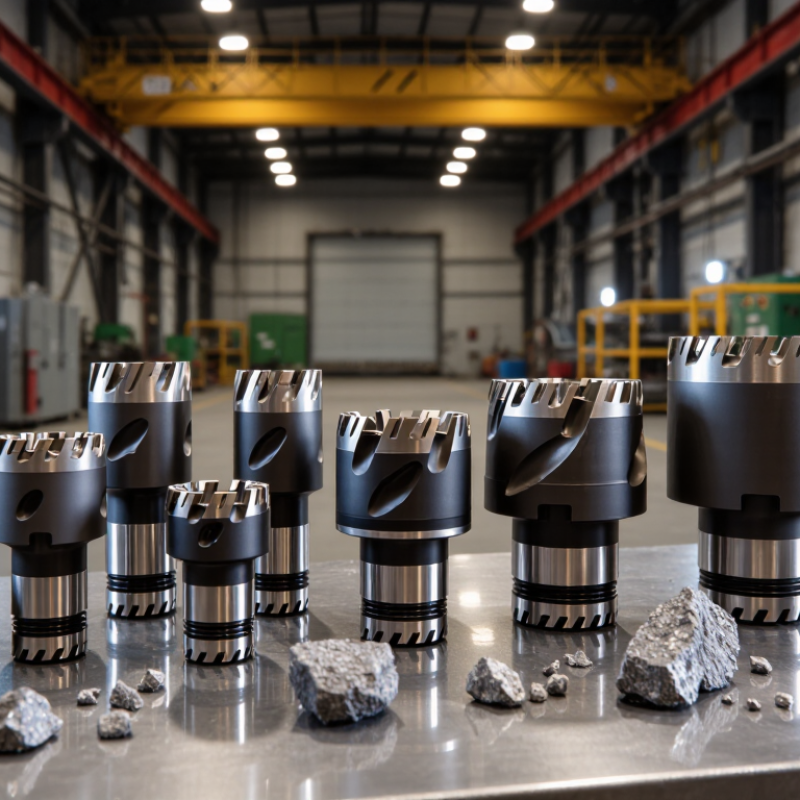
Masonry and hammer drill heads use carbide tips for brick, concrete, and stone. Their fluted bodies clear dust during impact drilling. For deeper geological sampling, core drill heads cut an annular path and preserve a cylindrical sample. Diamond-set versions handle hard formations, while carbide designs may cost less for softer ground.
I have seen purchasing teams focus too heavily on price. That can be a mistake. Ask about steel grade, tip attachment, hardness testing, runout, and coating thickness. Request inspection records and a sample before placing a large order. A CNC drill head needs accurate spindle alignment and stable bearings. A rock-drilling head needs tooth geometry matched to the formation. Share material, hole diameter, depth, machine speed, and cooling method with the manufacturer. Without these details, even a well-made head may perform poorly. I would also check packaging, batch identification, and replacement-part availability. These details seem minor. They are not.
Evaluating China’s leading drill head manufacturers requires more than comparing prices. The 2024 USGS Mineral Commodity Summaries confirms China’s major role in global mineral production. That scale supports strong demand for drilling components, but it does not guarantee consistent quality. Ask for measured runout, material certificates, heat-treatment records, and batch traceability. A serious supplier should explain testing methods clearly. Vague answers are warning signs.
Field experience matters. Request samples for controlled trials, then compare penetration rate, vibration, wear patterns, and service life. For rotary or rock-drilling applications, check thread accuracy, carbide retention, torque capacity, and compatibility with your equipment.
According to ISO 9001 principles, documented processes and corrective actions are more meaningful than a certificate displayed on a wall. The World Bank’s 2023 Logistics Performance Index also shows why delivery systems deserve attention; China ranked 19th globally, with a logistics score of 3.7.
Do not judge reliability from photographs alone. Visit the factory when possible, inspect CNC equipment, and review inspection reports from recent batches. A polished catalog can still mislead. I would also examine failure records, even when the supplier seems uncomfortable sharing them. That conversation reveals maturity. Price remains important, but an inexpensive drill head with unstable hardness can increase downtime, replacement labor, and project risk. Some evaluation decisions will remain imperfect. Record the assumptions, test results, and unanswered questions before signing a supply agreement.
When comparing top drill head manufacturers, examine technical standards before judging price or appearance. The right checks depend on the drilling material, machine speed, and connection type.
Request drawings showing diameter tolerance, concentricity, runout, thread accuracy, and contact-surface flatness. ISO 1101 can help define geometric tolerances clearly. For rotating tools, ask whether balance testing follows ISO 21940 principles. Small alignment errors can create vibration, heat, and uneven wear.
Material documents should identify the alloy, heat treatment, hardness range, and batch number. A proper EN 10204 3.1 inspection certificate offers useful traceability, but paperwork alone proves little. Ask for actual inspection records, not only a certificate copy. Check coating thickness, adhesion, and edge condition under magnification. Sharp edges should be consistent, without grinding burns or hidden cracks.
A reliable manufacturer should explain its sampling plan and final inspection equipment. Confirm whether gauges are calibrated and whether test results match the delivered batch. Trial testing matters too. Measure hole accuracy, tool life, and vibration under your real operating conditions. Factory claims may look impressive. Your material may behave differently. I would not ignore that weakness. Also review packaging, corrosion protection, replacement support, and response time for nonconforming parts. A supplier that accepts technical questions usually deserves closer attention.
| Evaluation Dimension | What to Check | Relevant Technical or Quality Standard | Recommended Acceptance Evidence | Priority |
|---|---|---|---|---|
| Product Application and Design Fit | Confirm whether the drill head is designed for rotary drilling, down-the-hole drilling, top-hammer drilling, reverse circulation, core drilling, or another application. Check compatibility with the drilling machine, shank, thread, hole diameter, rock type, and operating parameters. | Manufacturer’s approved technical drawing and customer specification. Dimensional tolerances may be defined using ISO 1101 for geometrical tolerancing. | Signed drawing, application data sheet, interface dimensions, recommended drilling parameters, and documented design review. | Critical |
| Material Traceability | Verify the steel grade, carbide grade, brazing alloy, or other material used in the body and wear elements. Heat number or batch identification should be traceable to incoming inspection records. | Material requirements should be stated in the purchase specification. Chemical composition can be verified by appropriate material analysis methods; quality systems should follow ISO 9001. | Mill test certificate, material certificate, batch number, heat-treatment record, and full traceability from raw material to finished product. | Critical |
| Hardness and Heat Treatment | Check hardness consistency, case depth where applicable, heat-treatment uniformity, and the absence of overheating, soft spots, quench cracks, or excessive brittleness. | ISO 6508 for Rockwell hardness, ISO 6507 for Vickers hardness, or an equivalent agreed testing method. | Hardness test report identifying test locations, equipment, method, calibration status, batch number, and measured values against the approved specification. | Critical |
| Mechanical Properties | For the drill body or critical load-bearing parts, assess tensile strength, yield strength, elongation, impact resistance, and fatigue-related requirements when specified by the application. | ISO 6892-1 for tensile testing of metallic materials. Impact testing may be specified using ISO 的148-1 where applicable. | Independent or in-house laboratory reports, test-piece identification, specimen orientation, test temperature, and results compared with the agreed material specification. | High |
| Dimensional Accuracy | Measure outside diameter, hole diameter, thread profile, shank dimensions, insert position, gauge length, concentricity, runout, and mounting interfaces. | ISO 1101 for geometrical tolerancing and the approved product drawing. Thread requirements should reference the applicable thread standard stated on the drawing. | Inspection report using calibrated gauges, coordinate-measuring equipment, thread gauges, or other suitable instruments. All critical dimensions should be recorded. | Critical |
| Surface Finish and Edge Condition | Inspect sealing surfaces, chip-flute areas, brazed zones, cutting edges, and threaded areas for burrs, laps, grinding burns, dents, sharp unintended edges, and excessive roughness. | ISO 21920-1 for surface texture specification and indication, where surface roughness is included in the drawing or purchase specification. | Visual inspection under controlled lighting plus surface-roughness measurements at specified locations using calibrated instruments. | High |
| Carbide Insert or Cutting Element Quality | Check insert grade consistency, dimensions, retention, orientation, brazing or mechanical fixation, edge integrity, and resistance to loosening during vibration and impact. | Customer-approved insert specification and manufacturing drawing. The acceptance criteria should define allowable cracks, chips, voids, position deviation, and braze coverage. | Incoming carbide inspection, brazing-process record, visual inspection, dimensional report, and sample destructive examination when required. | Critical |
| Welding and Brazing Quality | Evaluate joint penetration, wetting, voids, cracks, alignment, heat-affected zones, and post-braze cleanliness. The process should be controlled for temperature, time, flux, and cooling conditions. | Use a documented welding or brazing procedure. Non-destructive testing personnel and laboratories should be qualified where applicable; ISO 9712 may be used for personnel qualification. | Procedure qualification, operator qualification, furnace or torch records, joint inspection reports, and non-destructive testing records for critical joints. | Critical |
| Non-Destructive Testing | Screen for surface and internal defects such as cracks, shrinkage, inclusions, lack of bonding, and unacceptable porosity in safety- or performance-critical components. | Applicable methods may include visual testing, magnetic particle testing, penetrant testing, ultrasonic testing, or radiographic testing. The selected method must match the material and defect type. | Written NDT procedure, calibrated equipment record, qualified inspector, inspection coverage, acceptance level, and retained test results. | High |
| Balance, Concentricity, and Runout | Check rotational balance and radial runout where the drill head operates at high speed or is sensitive to vibration. Excessive runout can cause uneven wear, poor hole quality, and machine damage. | Acceptance limits should be established in the product drawing or customer specification based on operating speed and machine interface. | Runout measurement report, balancing record where applicable, fixture details, measurement points, and equipment calibration certificate. | High |
| Performance Testing | Compare penetration rate, drilling speed, service life, torque or impact response, vibration, hole straightness, and wear pattern under controlled conditions. | Use an agreed test protocol that defines rock or test medium, machine settings, water or air conditions, test duration, operator method, and failure criteria. | Factory or third-party test report with before-and-after measurements, operating parameters, sample identification, photographs, and repeatability data. | Critical |
| Quality Management System | Assess whether production, inspection, nonconforming-product control, corrective action, supplier management, and document control are systematically managed. | ISO 9001 quality management system certification, with certification scope covering the relevant manufacturing activities. | Valid certificate issued by an accredited certification body, audit summary, process-control plan, inspection plan, and corrective-action records. | High |
| Laboratory Competence | Check whether chemical, mechanical, dimensional, metallurgical, or non-destructive tests are performed by competent personnel using controlled methods and calibrated equipment. | ISO/IEC 17025 for testing and calibration laboratory competence, where an accredited laboratory is used. | Laboratory accreditation scope, test method, equipment calibration certificate, measurement uncertainty where relevant, and signed test report. | High |
| Inspection Sampling and Lot Control | Confirm how production lots are defined, how samples are selected, and which characteristics receive 100% inspection versus sampling inspection. | ISO 2859-1 may be used for attribute-based sampling plans when agreed by the buyer and supplier. Critical characteristics may require 100% inspection. | Approved inspection and test plan, sampling level, acceptance number, lot definition, inspection records, and disposition of rejected items. | High |
| Corrosion Protection and Packaging | Check rust prevention, protective coating, thread protection, moisture control, impact protection, packaging strength, labels, and storage life. | Packaging and preservation requirements should be stated in the purchase specification. Environmental requirements may reference ISO 9227 for agreed salt-spray testing when a coating test is necessary. | Packaging specification, coating or preservation record, transport test evidence where required, product label, batch identification, and storage instructions. | Medium |
| Documentation and Change Control | Verify control of drawings, revisions, bills of materials, process changes, substitute materials, tooling changes, and customer notifications. | ISO 9001 document-control and change-control requirements, supplemented by the customer’s engineering-change procedure. | Controlled drawing revision, change-notification process, engineering-change records, approval signatures, and retained production history. | High |
| Warranty and Corrective Action | Review warranty duration, wear-related exclusions, failure analysis capability, response time, replacement policy, and corrective-action effectiveness. | Contractual quality agreement and ISO 9001 corrective-action requirements. Failure analysis should be based on documented evidence rather than visual assumptions alone. | Written warranty terms, complaint-response procedure, root-cause analysis, corrective-action report, replacement policy, and historical quality metrics. | High |
When comparing China’s top drill head manufacturers, price is only the opening figure. Ask what the quote includes: carbide inserts, shank inspection, packaging, and export documents. A low unit price may exclude trial samples or tooling adjustments. Request a written breakdown with minimum order quantity, replacement terms, and payment stages. I have found that a slightly higher price can be safer when tolerance reports arrive with every batch. Still, “premium” does not prove better performance. Test two samples in the same material, speed, and feed conditions. Record hole diameter, vibration, edge wear, and cutting time. Keep the data, not just sales promises.
Support should be measured before a purchase problem appears. Can an engineer answer questions about alloy hardness, coolant flow, and recommended cutting parameters? Check response times through email or video calls. Ask for drawings, inspection records, and a clear method for handling defective parts. Vague support becomes expensive during machine downtime. I once underestimated this point. It delayed a production decision. Delivery also needs more than a shipping date. Confirm production lead time, inspection time, packing method, and the handoff point for freight. Ask whether partial shipments are possible when one size is delayed. A realistic schedule is better than an attractive promise. Build a small buffer for customs clearance and seasonal congestion. Then compare the full landed cost, service evidence, and delivery risk together.
Use a weighted purchasing scorecard to compare price, technical support, delivery reliability, customization capability, and warranty service before selecting a supplier.
The index is normalized to 100 points. Lower pricing improves the price score, while faster confirmed lead times, stronger engineering assistance, reliable delivery performance, and longer warranty coverage increase the other scores. Buyers should verify these indicators with quotations, sample testing, service agreements, and production schedules.