Pawsome-Specializing in vet health products since 2015
Choosing the right Cutting Wire is less about picking the strongest option and more about matching the wire to the material, machine, and finish you need. A wire suited to a delicate foam cut may perform poorly on a dense block. Even a small mismatch can leave rough edges, slow production, or cause frequent wire changes. The details matter.
For this introduction, the quoted specialist is a fictional composite, not a real or independently verified source. Mara Voss, a composite cutting-wire specialist, puts the principle this way: “The best wire is the one that fits the cut, not the one with the biggest specification.” It is a useful reminder, though real operating conditions can complicate any neat rule. Wire material, diameter, tension, temperature, and feed speed all influence results. A thin wire may create a narrow kerf, but it may also be less durable in demanding work. There is no universal best choice.
This guide outlines how to compare wire types and specifications, then connect them to your application. It also considers practical checks, such as cut quality, equipment compatibility, and replacement frequency. Start with the material and the result you want. Then test a suitable option on a small sample, recording the settings and finish. A careful trial often reveals what a product sheet cannot.
What Is Cutting Wire and How Is It Used?
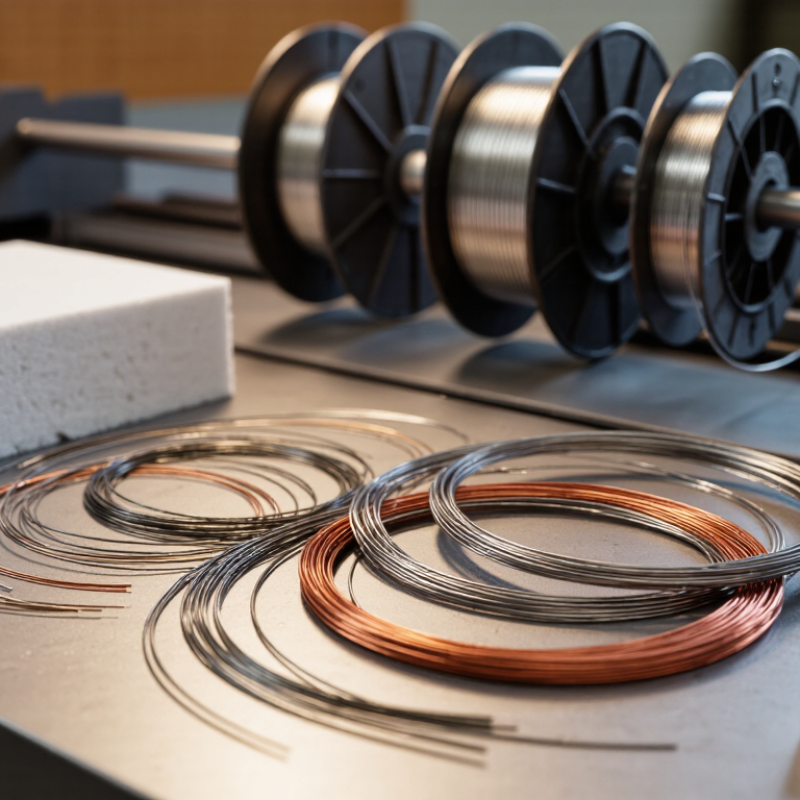
Cutting wire is a thin, tensioned wire used to separate material with a controlled, narrow cut. The exact method depends on the wire and the material. A heated wire can slice through foam by softening it along the cut line. In workshops, abrasive or diamond-coated wire can cut brittle materials such as glass and stone. Electrical discharge machining uses a fine wire and electrical energy to shape conductive metals.
The wire’s diameter, coating, tension, and cutting speed affect the result. For example, a taut wire can make a straighter cut, while excess force may cause it to bow or snap. Operators often test settings on a spare piece first. Small changes matter. Cutting wire is useful for detailed shapes, tight curves, and reduced material waste, but it is not automatically the right tool for every job. Heat, dust, and sharp edges may require suitable guards and protective equipment.
Tips: Match the wire to the material, not just the desired shape. Check the manufacturer’s operating guidance and inspect the wire for kinks or wear before use. Keep the workpiece steady, and avoid pulling harder when a cut slows; the cause may be a dull wire or an unsuitable setting. Results can still vary with material thickness and temperature, so a test cut is worth the extra minute.
In wire electrical discharge machining (EDM), a thin, electrically conductive wire acts as an electrode to cut electrically conductive materials. Wire diameter affects the achievable cut width and is selected according to the job’s precision and cutting requirements.
The chart shows commonly available nominal wire diameters and general use cases. Actual suitability depends on the machine, material, and desired cut quality.
The right wire material depends on what you are cutting, the required finish, and the working conditions. For soft foam or wax, a resistance wire can create a clean cut when its temperature and tension are controlled. Stainless steel wire offers better corrosion resistance in damp environments, while high-carbon steel can provide useful strength for demanding mechanical cutting. These materials are not interchangeable. A wire that performs well on foam may be unsuitable for abrasive or hard stock.
Tips: Check the material’s tensile strength, heat tolerance, and corrosion resistance. Match its diameter to the tool and the cut. A thicker wire may last longer, but it can leave a wider kerf. Small details matter.
Before choosing, consider the workpiece and how often the wire will be used. Abrasive materials can wear a fine wire quickly. Heat-sensitive materials may deform if the wire runs too hot. Read the equipment specifications, then test a short sample under realistic conditions. Watch for fraying, uneven cuts, or excessive heat. I have found that a technically suitable wire can still disappoint when tension is poorly adjusted. There is no perfect choice for every task; a modest test often reveals what a chart cannot.
How to Choose the Right Cutting Wire?
Wire diameter changes how a cutting wire behaves under load and heat. A thicker wire is generally stronger and less likely to stretch, but it may need more power to reach the required cutting temperature. A thinner wire can heat quickly and make a narrow cut, yet it is easier to damage or deform. The exact result depends on the wire material, power supply, and the material being cut. Small changes matter. For example, a wire that cuts foam cleanly at one setting may leave a rough edge when the feed rate increases.
Length matters too. A longer wire usually has greater electrical resistance, so the same power setting may produce less heat along its span. It can also sag more unless tension is managed carefully. A short wire is often easier to keep steady, but may not suit a wide workpiece. Check the equipment’s rated wire range before changing either dimension. Then test a small sample and inspect the cut edge, wire tension, and temperature. It is tempting to assume that more power fixes a slow cut. Not always. I would reconsider the setup if the center cuts differently from the ends; uneven tension or heat may be the real issue.
This guide focuses on wire electrical discharge machining (wire EDM). Actual performance depends on the machine, workpiece material, settings, and the wire manufacturer’s specifications.
| Selection factor | Typical range or option | Effect on cutting | When it may be suitable | Practical trade-off |
|---|---|---|---|---|
| Wire diameter | About 0.10–0.30 mm; 0.25 mm is a common general-purpose size | Diameter contributes to the cut width (kerf), together with the electrical discharge gap. A smaller wire can make narrower cuts and access smaller features; a larger wire is generally more resistant to breakage. | Choose a smaller diameter for fine details, small radii, or narrow slots. Choose a larger diameter when the geometry and machine setup allow it and greater wire robustness is useful. | Fine wire can be more sensitive to flushing, tension, and cutting conditions. The smallest available diameter is not automatically the best choice. |
| Wire diameter and cutting speed | Compare diameters within the range supported by the machine and process | Diameter alone does not determine cutting speed. Speed also depends on factors such as workpiece thickness and material, discharge settings, flushing, and wire type. | Use the machine’s recommended process settings and wire specifications when choosing a diameter for a particular job. | A larger diameter may offer greater mechanical robustness, but it does not guarantee a faster cut or a better finish. |
| Wire length on a spool | Varies by spool size, wire diameter, and wire material; check the stated length or net weight | More usable wire supports longer uninterrupted runs and fewer spool changes. With the same wire and machine settings, spool length does not directly change the kerf or cutting accuracy. | Choose a longer supply for long jobs, production runs, or situations where reducing changeovers is valuable. | Confirm that the spool format and dimensions are compatible with the machine’s wire-feeding system. |
| Wire length required per job | Depends on wire-feed rate, cutting time, threading, and setup or restart needs | Wire EDM continuously feeds wire during cutting, so consumption is related to feed rate and operating time rather than simply the length of the workpiece. | Estimate consumption using the machine’s feed settings and expected cutting time, then allow for threading and normal process interruptions. | Actual usage varies by machine and operating conditions; use production records or the machine manual for a reliable estimate. |
| Workpiece thickness and geometry | Assess the full thickness, slot width, corner radius, and required detail | Thick sections and tight geometry can impose different demands on wire stability, flushing, and machining settings. Wire diameter must fit the required feature and permitted kerf. | Check the machine’s capacity and process recommendations for the workpiece material and geometry before selecting wire. | Changing wire diameter may require adjustments to offsets and process settings; verify dimensions with a test cut when accuracy is critical. |
| Final selection | Match diameter, wire type, and spool format to the job and machine | The right choice balances feature size, dimensional requirements, process stability, and the amount of uninterrupted cutting required. | Start with the machine maker’s approved wire specifications and the job’s required kerf, finish, and tolerance. | Do not compare wire length alone: confirm the stated usable length, spool compatibility, and recommended operating conditions. |
Note: The diameter range shown is a general wire-EDM reference, not a universal specification. Always verify compatibility and process parameters with the machine documentation and the wire supplier’s technical data.
Which Operating Conditions and Tool Requirements Matter?
Start with the material, thickness, and shape you need to cut. A thin wire may suit delicate work, while thicker stock can require greater tensile strength. Check the wire’s rated load and compatibility with your tool before use. A close fit matters: incorrect tension can cause poor cuts, excessive wear, or breakage. Heat changes everything. For heated cutting, confirm that the wire tolerates the operating temperature and that the tool controls heat consistently. For unheated cutting, focus on hardness, edge wear, and the force needed to move through the material.
Consider the work environment, too. Dust, moisture, and repeated bending can affect wire life. If the tool runs for long periods, choose a wire suited to continuous operation and follow the tool maker’s limits. Watch for uneven tension or fraying during setup; small signs can point to a mismatch. It is tempting to choose the strongest option, but a very stiff wire may be harder to control in fine, detailed cuts. I’d treat the first test as a check, not proof: materials and settings can vary more than expected.
Tips: Match wire diameter to the tool’s guides. Keep tension even. Test on a spare piece, then inspect the cut and wire for heat marks, bends, or wear.
Matching cutting wire to an application starts with the material being cut. Foam, wax, and soft insulation usually need less force than dense or abrasive materials. Check the material’s thickness, density, and surface finish requirements. A wire that cuts cleanly through a thin foam sheet may struggle with a thick block. Test a small offcut first.
Next, consider wire diameter, tension, and operating temperature. Thicker wire can resist breakage, but it may leave a wider kerf. Fine wire can create detailed shapes, yet it needs careful handling and consistent tension. For heated cutting, match the temperature to the material and feed speed. Too much heat can cause rough edges, fumes, or unwanted melting. Start low.
The tool and work area matter, too. Hand cutting calls for a wire that stays manageable across the intended span; machine cutting requires compatible tensioning and stable feed. Keep the wire straight, inspect it for kinks, and replace it when wear appears. I’ve found that a quick trial often reveals what a spec sheet misses. Still, one test is not enough for every batch. Record the settings, then check the cut again when material thickness or ambient conditions change.